
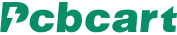


Design the panel around what the SMT line has to grip, locate and inspect: tooling strips (we recommend 7.0 mm wide) carrying at least three 1.0 mm fiducials and 3.0 mm tooling holes, V-cut only for units that share a size and straight edges, and tab routing for everything else. Material utilization on the fab panel comes second. An array that is cheap to fabricate but hard to carry, locate or depanel will cost you more in assembly than the laminate you saved.
Why should the assembly line drive your panel design?
Because the line is the stricter customer. A board house looks at a production sheet and asks how many units fit. The assembly line asks whether the panel rides a conveyor, locates under the printer and placement head, and comes apart afterward without cracking anything. Those two questions often produce different layouts.
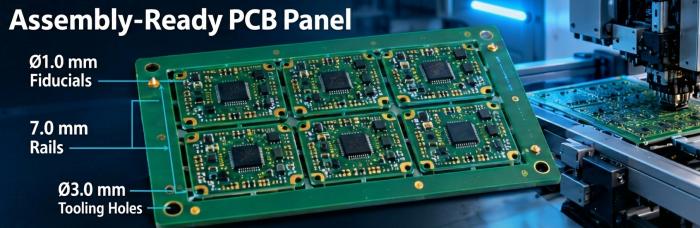
The size limits show the gap. Standard FR4 boards can be fabricated from 6×6 mm up to 600×700 mm, but an assembly panel runs between 50×50 mm and 310×410 mm, as listed on our Panel Requirements page. A 20 mm sensor board should not travel alone, and a 500×600 mm fab array is not an assembly panel. If you send us a single-board file, we can panelize it to your requirements. If you already have a panel, we build from your panelized file.
The page gives three reasons to panelize: fabrication efficiency, lower assembly labor per board, and quality control. The third one is easy to underrate. One set of fiducials, one program and one handling step cover every unit on the panel, so setup and placement offsets are shared rather than repeated per board.
The failure we run into most often is an array exported straight from a fab layout: units touching the outer edge, no rails, and fiducials only inside each unit. It fabricates fine. On the line, there is nothing for the conveyor to ride and nowhere to put panel-level marks.
How wide should rails be, and when do you need them?
Our recommended tooling strip width is 7.0 mm, and you need rails whenever the units cannot be carried by their own edges or cannot hold the marks themselves. The rails do three jobs: they give the conveyor an edge with nothing hanging over it, they carry the panel fiducials, and they hold the tooling holes.
The 7.0 mm figure is closer to arithmetic than preference. A 3.0 mm tooling hole in the middle of the strip leaves 2.0 mm of material on each side, and the 1.0 mm fiducials also sit in the middle of the strip. Squeeze the strip below that and either the hole or the mark has to move somewhere less useful.
Rails earn their space when:
components sit close to the unit edge, or overhang it
the outline is irregular, rounded or has cutouts
the unit is small enough that it would not be stable alone
A clean rectangular board with nothing near its edges is the only case where we would even discuss dropping the rails, and we would decide that board by board. If that is your situation, confirm with our engineering team before you finalize the array.
Spacing between units is separate from rail width and depends on how you separate them. The numbers are in the comparison table below.
Global vs local fiducials
Global fiducials are panel-level marks. Our requirement is at least 3 per panel, 1.0 mm in diameter, placed in the middle of the tooling strips. Two marks fix offset, rotation and scale along one line; the third lets the machine also see skew across the panel.
The page also gives positions: the marks on the left are 10.0 mm from the board edge and the ones on the right are 15.0 mm from the right edge. The two numbers differ, and we would copy them as written instead of mirroring the layout for symmetry.
Local fiducials sit on each unit, close to fine-pitch parts such as BGAs and QFNs. The page does not give local fiducial dimensions, so for size, copper clearance and mask opening, confirm with our engineering team. What we can say as a design judgment: do not rely on panel-level marks alone for fine-pitch parts. Units can sit slightly differently from the panel nominal after routing and handling, and a local mark lets the machine correct for the unit it is actually placing.
Keep silkscreen, traces and other copper features out of the area around any mark. The exact clearance is another thing to confirm with our engineering team.
Tooling holes
Our recommendation is 3.0 mm diameter holes in a 7.0 mm wide tooling strip, with at least 5.0 mm between the hole and the edge of the board. Panel-level location and support tooling pick up on these holes, so treat them as a datum and not as a place to drill wherever there is room.
Two things we check on incoming panel data. First, the holes are actually on the rails and not inside a unit outline, where depaneling would remove them. Second, nothing else sits in the strip that could collide with a locating pin: stray test points, panel labels, or a fiducial moved too close.
Plated or non-plated, and positional tolerance, are not specified on the page. Confirm with our engineering team.
V-score vs tab routing, and components near the edge
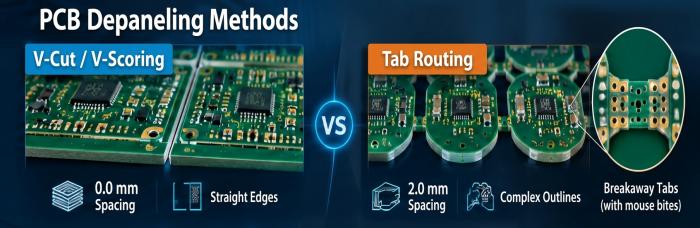
Use V-cut when every unit is the same size with straight edges and the whole panel can be scored in continuous lines. Use tab routing when anything breaks that pattern. The V-score tool cuts through the entire panel in one pass and cannot stop partway, so a panel with units of different sizes is a tab-routing job. The page says so directly.
| Items | V-cut / V-groove | Tab routing with breaking holes | Tab routing with tabs |
|---|---|---|---|
| Spacing between units | 0.0 mm | 2.0 mm | 2.0 mm |
| Unit shapes | Same-size units with straight edges | Any outline | Any outline |
| Breakaway detail | Score line, continuous across the panel | Holes 0.3–1.0 mm, spacing between holes ≥0.25 mm, about 5–6 holes per tab | Tab width 1.0 mm |
| Best fit | Dense rectangular arrays | Outlines with corners, curves or cutouts | Same, where a solid tab is preferred |
A panel that combines V-cut and route also needs 2.0 mm between units, so adding one routed edge to a V-cut array removes the 0.0 mm spacing advantage. If you want the density of V-cut and your board has rounded corners, check whether the corner radius really needs to be there before you commit to the combined approach.
Breaking holes and tabs both leave small stubs on the board edge after separation. If the board slides into a slot or a rail in your enclosure, tell us the mating dimension so the tab location is chosen to stay clear of it. The V-cut route has its own quirk: for thinner finished boards, scoring may only be possible from one side. The thickness at which that applies is not stated consistently enough for us to quote a number here, so confirm with our engineering team.
On components near the edge, the page gives no keep-out distance and we are not going to invent one. The right number depends on part type, package size and the separation method. What we ask for in review is simple: connectors and other parts that overhang the board outline push you toward tab routing, and anything fragile near a score line or tab should be flagged on the drawing.
Depaneling stress and how to avoid cracked parts
Ceramic chip capacitors are the usual victims, followed by parts with brittle terminations or solder joints under them such as large BGAs and QFNs. The cause is board flex at the moment of separation, and the strain is highest closest to the score line or tab.
What helps, in order of how often it matters:
Keep ceramic capacitors, resonators and large area-array parts away from score lines and tabs. Give them as much distance as the layout allows.
Put tabs where no fragile part is nearby, and avoid placing tabs directly beside parts that you know are strain-sensitive.
Do not plan on snapping populated boards apart by hand. If your design depends on hand-breaking, say so in your package so the separation method can be reviewed.
Ask for review early. Moving a capacitor before layout freeze takes minutes. Finding it after the first cracked part takes a rebuild.
We would rather catch this before release, which is what the free DFM check is for. Send the panel drawing with the board files and mark the parts you consider strain-sensitive.
Panel stiffness is a related issue. A panel with heavy parts on one side, or large cutouts, can bow when it is heated, and the more of the panel that is V-scored, the less material is holding it together. If your panel has either feature, mention it in the notes and confirm support requirements with our engineering team.
What to include with your panel data
Send the panel and the unit data together, and make it obvious which is which. A package that works well for us:
Gerber files for the panelized array, or single-board files if you want us to panelize
A panel drawing showing overall dimensions, unit count and arrangement, spacing between units and rail width
The separation method for each edge: V-cut, tab routing, or a mix, with tab positions and the breaking-hole pattern
Locations and diameters for fiducials and tooling holes
Any unit that is rotated or mirrored in the array
Pick-and-place (centroid) data, stating whether the origin is the panel or a single unit
Parts near edges, overhanging parts and strain-sensitive parts, marked on the drawing
The origin point and the rotated units cause more delay than the geometry does. Placement data that refers to a single board while the file contains a panel is easy to miss until the first program is checked.
FAQ
Should the fab panel and the assembly panel be the same?
Ideally, yes. A bare-board maker optimizing for utilization may leave no rails, use different spacing, or produce a panel larger than 310×410 mm, and then you are re-panelizing or re-ordering. Settle the panel design with assembly in mind before bare boards are ordered.
Can I put two different board designs on one panel?
The layout side is workable with tab routing, since V-cut cannot handle units of different sizes. Whether it makes sense for assembly depends on the BOMs, programs and how you plan to separate and test the units, so confirm with our engineering team before you design it.
Is the 2.0 mm spacing for tab routing a hard limit?
It is what our Panel Requirements page asks for. If your design needs something else, send the drawing and our engineering team will review it. We would not assume it is acceptable without that.
Can a board with rounded corners or cutouts be V-scored?
Only along straight lines that cross the whole panel. Curved outlines and internal cutouts need routing, which brings you to the 2.0 mm spacing for a combined panel.


